Turnkey — design, supply, installation, commissioning · 2020
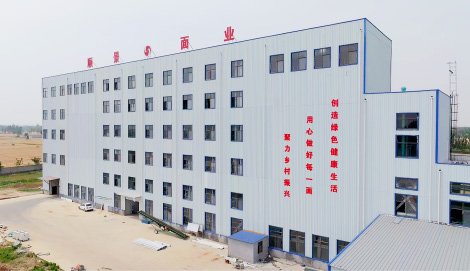
Shufu 200 t/d flour plant
A 200 t/d plant with a double-purifier bank feeding two high square plansifters, and automatic proportioning across three wheat origins to hold a 12.3% protein specification year-round.
- 60+ years manufacturing
- 10–500 t/d capacity range
- 100+ patents
- Turnkey commissioning
Capacity
200 t/d
Installed power
690 kW
Specific power
68–72 kWh/t
Flow sheet
4B5M1S1T
Purifiers
2 banks, 6 sections each
Blending
3 origins, automatic
疏附 200 吨面粉厂 · Shufu County, Kashgar Prefecture, Xinjiang, China
The brief
The client supplies flour to a regional bakery group under an annual contract that specifies 12.3% protein at 14% moisture basis, with a tolerance of ±0.3%. Local wheat runs 10.8–11.6%, so the specification cannot be met without imported high-protein wheat.
The plant therefore had to be designed around blending from the start, not as an afterthought. That single requirement shaped the silo configuration, the intake layout and the control system.
What constrained the design
Four constraints that shaped the plant more than the capacity figure did.
Contractual protein specification
Holding ±0.3% protein requires continuous proportioning, not batch blending. Two 1,000 t silos for local wheat and one 600 t silo for imported spring wheat, each with a variable-speed weigh-belt feeder, feeding a common collecting conveyor under PLC ratio control.
Two purifier passes
The bakery specification requires patent flour at 0.45% ash, which is at the low end for a 200 t/d plant. Two purifier banks in series were specified rather than one, allowing the semolina stream to be re-cleaned before the reduction passages.
Restricted site
The available plot was 42 × 30 m with an existing office block on the north side. A 40 × 8 × 18.5 m storey-typed building was fitted by orienting the intake from the east and the packing hall to the south, keeping truck traffic away from the office.
What was built
| Intake | 60 t weighbridge, 25 t/h receiving capacity, roofed pit with automatic sampler. Two-hour buffer bin ahead of cleaning. |
|---|---|
| Blending | Three silos with weigh-belt feeders, PLC ratio control, belt scale verification. Moisture-corrected blending on dry matter. |
| Cleaning | Single 12 t/h line: self-balancing screen, gravity destoner, two horizontal scourers, magnetic separation, automatic dampening to 16.2%. |
| Tempering | Four bins, 18-hour minimum. Wheat moisture measured at bin entry and exit. |
| Milling | 4B5M1S1T on six FMFQ(S) double roller mills. Twin 1B configuration for the higher break capacity. |
| Sifting | Two FSFG high square plansifters, 44 m² total — 0.88 t/d per m². |
| Purification | Two FQFD purifiers in series, 6 sections each, with independent aspiration. |
| Control | PLC with HMI, bin level radar, moisture control, roll gap monitoring, 12-month historian. |
Measured outcome
Performance acceptance at 203 t/d, 75.8% extraction, 0.46% patent ash, 70.1 kWh/t. Blend protein held at 12.28% average over the 72-hour test with a range of 12.21–12.34%.
Over the first 18 months the plant held the bakery contract specification on every delivery. Two loads were diverted to lower-grade product when imported wheat was unavailable for three weeks — the blending system made that a commercial decision rather than a quality failure.
Specific power settled at 69.5 kWh/t after six months of stabilisation, against a design figure of 70.
What we would do differently
The honest section. Every project teaches something that was not in the specification.
- Continuous proportioning was the correct choice over batch blending. The batch alternative would have needed a 4-hour buffer bin and produced a transition slug at every switch — at 200 t/d that is 33 t of off-specification flour per switch.
- Two purifier banks in series added 6% to equipment cost and delivered the 0.45% ash specification. One bank would have produced 0.52–0.55% ash, which would have failed the contract.
- The PLC historian was specified as an option and included. It identified a 1.2% extraction drift over four months caused by slow sifter screen blinding — a loss that would otherwise have run until the annual shutdown.
Next step
Planning a plant of this size?
Send us your target capacity, wheat specification and site constraints. We will tell you what a plant like this one would need — and what we would change if we built it today.